2026 Top Ropes for Tower Cranes How to Choose?
Choosing Ropes For Tower Cranes is not a catalogue exercise. The rope must handle the crane’s reeving pattern, lifting duty, drum geometry, and exposure to abrasion. A small wire break near a sheave can matter. So can a rope that looks sound but has endured repeated bending. The right choice starts with the crane manufacturer’s specifications, then checks the rope’s construction, strength, and inspection requirements.
Industry guidance makes these checks concrete. ISO 4309:2017 sets out care, maintenance, inspection, and discard criteria for crane wire ropes. In the United States, OSHA’s 29 CFR 1926.1413 addresses wire-rope inspections on construction cranes. The U.S. Bureau of Labor Statistics reported 1,075 fatal work injuries in construction and extraction occupations in 2023; that figure is not rope-specific, but it underlines why equipment decisions deserve care. Small details matter.
Wire-rope engineer Klaus Feyrer’s book, Wire Ropes: Tension, Endurance, Reliability, examines how loading and repeated bending affect rope performance. A practical paraphrase of that engineering perspective is simple: do not judge a rope by breaking strength alone. This is a paraphrase, not a verified direct quotation. In this guide, we compare rope constructions, rotation resistance, and fit for common tower-crane duties, while noting where site conditions change the answer. There is no universal “top” rope. The best option is the one specified for the crane and suited to its real working cycle.
What Tower Crane Ropes Do and How They Are Classified
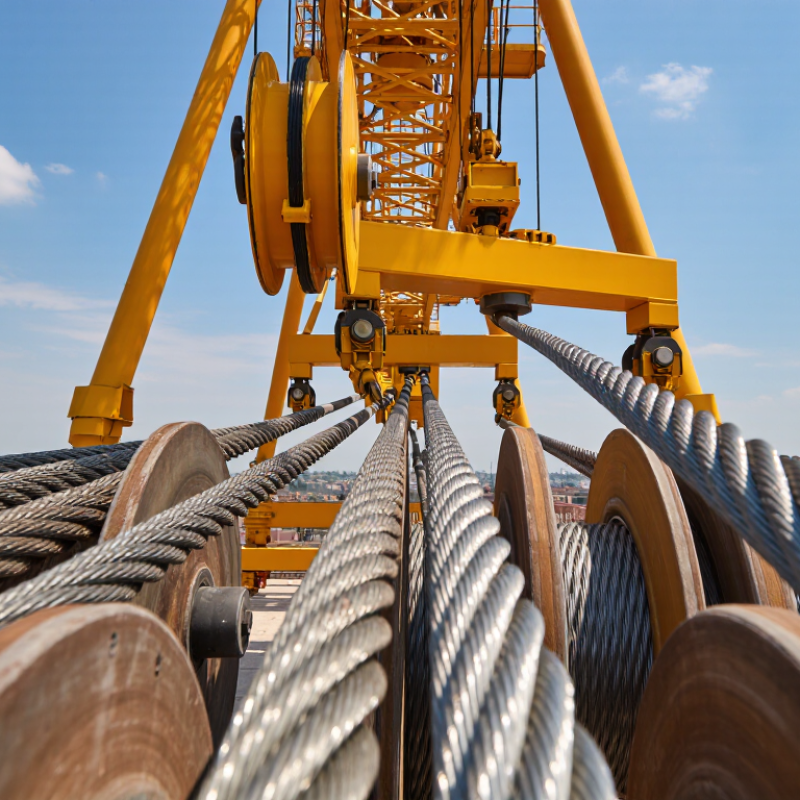
On a tower crane, wire ropes carry lifting forces between the hoist, sheaves, drum, and suspended load. They may also operate luffing systems or move a trolley, depending on crane design. Their condition affects smooth movement, load control, and safe operation. A rope is not simply “strong” or “weak.” Its construction matters.
Ropes are commonly classified by core type, strand arrangement, lay, and resistance to rotation. Fibre-core ropes are flexible, while independent wire-rope cores generally provide greater structural support under pressure. Rotation-resistant designs help limit load twisting, especially with long falls, but they need careful handling. Some ropes have compacted strands or protective coatings for particular wear or corrosion conditions. Small details matter. Selection also depends on rope diameter, crane reeving, drum grooves, working load, and duty cycle. Check the crane documentation and rope inspection criteria before replacement; a nominally similar rope may behave differently. In real service, classifications can overlap, and field conditions are rarely as neat as a chart suggests. Regular inspection for broken wires, deformation, corrosion, and diameter loss helps identify problems early.
Which Rope Materials and Constructions Suit Crane Duties
Tower-crane hoist ropes face repeated bending, high tension, and abrasion against sheaves. Steel wire rope remains a practical choice because its construction can balance flexibility and wear resistance. The Wire Rope Technical Board’s Wire Rope Users Manual describes common 6×19 and 6×36 rope families: six strands, with nominally 19 or 36 wires per strand. Finer wires generally bend more readily, while larger outer wires usually tolerate abrasion better. That trade-off matters.
For frequent lifting, a rotation-resistant steel rope can help control load spin, but its layered construction needs careful inspection and compatible reeving. An independent wire-rope core generally supports the strands better under crushing pressure than a fiber core. Synthetic ropes are lighter, yet heat, sharp edges, and sheave compatibility can limit their use on tower cranes. Check the rope maker’s technical specifications against the crane manual; matching diameter alone is not enough. A rope can look sound.
Inspection should consider broken wires, corrosion, deformation, and diameter change. ISO 4309:2017 sets out inspection and discard guidance for crane wire ropes, emphasizing multiple indicators rather than one visual clue. Track rope condition and service history, and ask a qualified person to assess uncertain damage. In practice, the best construction is the one suited to the crane’s reeving, duty cycle, and inspection regime—not simply the strongest listed option. I would not treat a single specification as a complete answer.
How to Match Rope Specifications to Crane and Load Requirements
Matching rope specifications to a tower crane begins with its approved reeving arrangement, hoist speed, drum dimensions, and load chart—not diameter alone. Check rope construction, nominal diameter, grade, core, and minimum breaking force against the crane manufacturer’s requirements. A 20 mm rope is not automatically suitable: construction and fleet angle affect how it bends, wears, and fits the drum grooves. Include the lifted load, hook block, and rigging in the operating calculation.
ISO 2408:2017 specifies requirements for steel wire ropes, including minimum breaking force. ISO 4309:2017 covers inspection and discard criteria, including broken wires, diameter reduction, corrosion, and deformation. These checks matter because discard limits vary with rope construction and operating conditions. Repeated bending over small sheaves can accelerate fatigue. A spreadsheet may make selection look exact; actual wear is less tidy, so inspection records still matter.
Tips: Confirm the rope’s certificate and construction match the crane documentation. Measure the drum groove and sheave diameter, then inspect for crushing or birdcaging after unusual loading. Record rope diameter at consistent points. If the configuration has changed, pause and get a qualified lifting professional to verify compatibility.
2026 Top Ropes for Tower Cranes: How to Choose?
Match the hoist rope to the crane’s reeving arrangement and the load it must lift. This chart shows the ideal rope-line tension for a 100 kN suspended load at different numbers of supporting rope parts.
How to read it: In an ideal reeving system, line tension equals load divided by the number of supporting rope parts. Actual tension can be higher because of sheave friction, acceleration and other operating effects. Use the crane manufacturer’s specifications and applicable standards to verify rope construction, diameter, minimum breaking force and safety factor.
How to Compare Top Tower Crane Rope Options in 2026
How to Compare Top Tower Crane Rope Options in 2026
Compare ropes against the crane’s reeving, drum groove, lift height, and duty cycle—not breaking strength alone. A rope that looks stronger on paper may wear faster if it repeatedly bends over small sheaves. Check construction, diameter tolerance, minimum breaking force, core type, and rotation behavior on the supplier’s certificate. Steel cores generally resist crushing better; fiber cores can offer greater flexibility. Neither is automatically the better choice.
ISO 4309:2017, Cranes—Wire ropes—Care and maintenance, inspection and discard, bases discard decisions on factors including broken wires, diameter loss, corrosion, and deformation. Its thresholds depend on rope construction and operating arrangement; there is no single safe broken-wire count for every tower crane. Ask for the applicable inspection table, plus documented test results. Then compare lubrication and inspection access. Small details matter.
For high-cycle lifting, assess fatigue performance and compatibility with the crane maker’s specified reeving. For long, freely suspended loads, review rotation resistance and the required end connections. I’d also ask how the rope behaves after installation, not just how it tests new. That detail is often missed. A neat specification sheet cannot predict every site condition, so record baseline diameter and surface condition before service.
How to Verify Rope Quality, Compatibility, and Service Life
A tower-crane rope is not a “fits the drum” purchase. Match its diameter, construction, lay, strength grade, and rotation characteristics to the crane maker’s specifications. Then check the reeving, sheave grooves, drum capacity, and end terminations. A mismatch can cause poor spooling, accelerated wear, or uncontrolled rotation. Keep the rope certificate and verify its stated breaking force and traceability against the order. Small paperwork gaps matter.
Inspect the rope under safe conditions, including areas hidden at sheaves and drum crossover points. Look for broken wires, corrosion, crushing, kinks, and diameter loss. OSHA’s US construction-crane criteria identify six randomly distributed broken wires in one rope lay, or three in one strand in one lay, as removal triggers for running ropes (29 CFR 1926.1413). These are not universal limits; rope type and local requirements matter. ISO 4309:2017 also provides inspection and discard guidance for crane wire ropes. A clean surface can still conceal internal damage.
Service life has no dependable calendar answer. Loads, duty cycles, reeving, lubrication, environment, and handling all change it. Record inspections, operating hours, repairs, and measured diameter at consistent points. Compare results over time, not just against a new-rope reading. Salt air or abrasive dust? Inspect more closely. One awkward truth: a rope may reach discard condition sooner than expected, even with careful maintenance.